A different forming route

One-piece injection-compression molding for isolator gloves.

Kingsure forms the complete glove from solid rubber compound inside dedicated closed tooling. The route removes the repeated open-bath coating step and sharply reduces reliance on the solvent preparation systems used by solvent-based dipping processes.
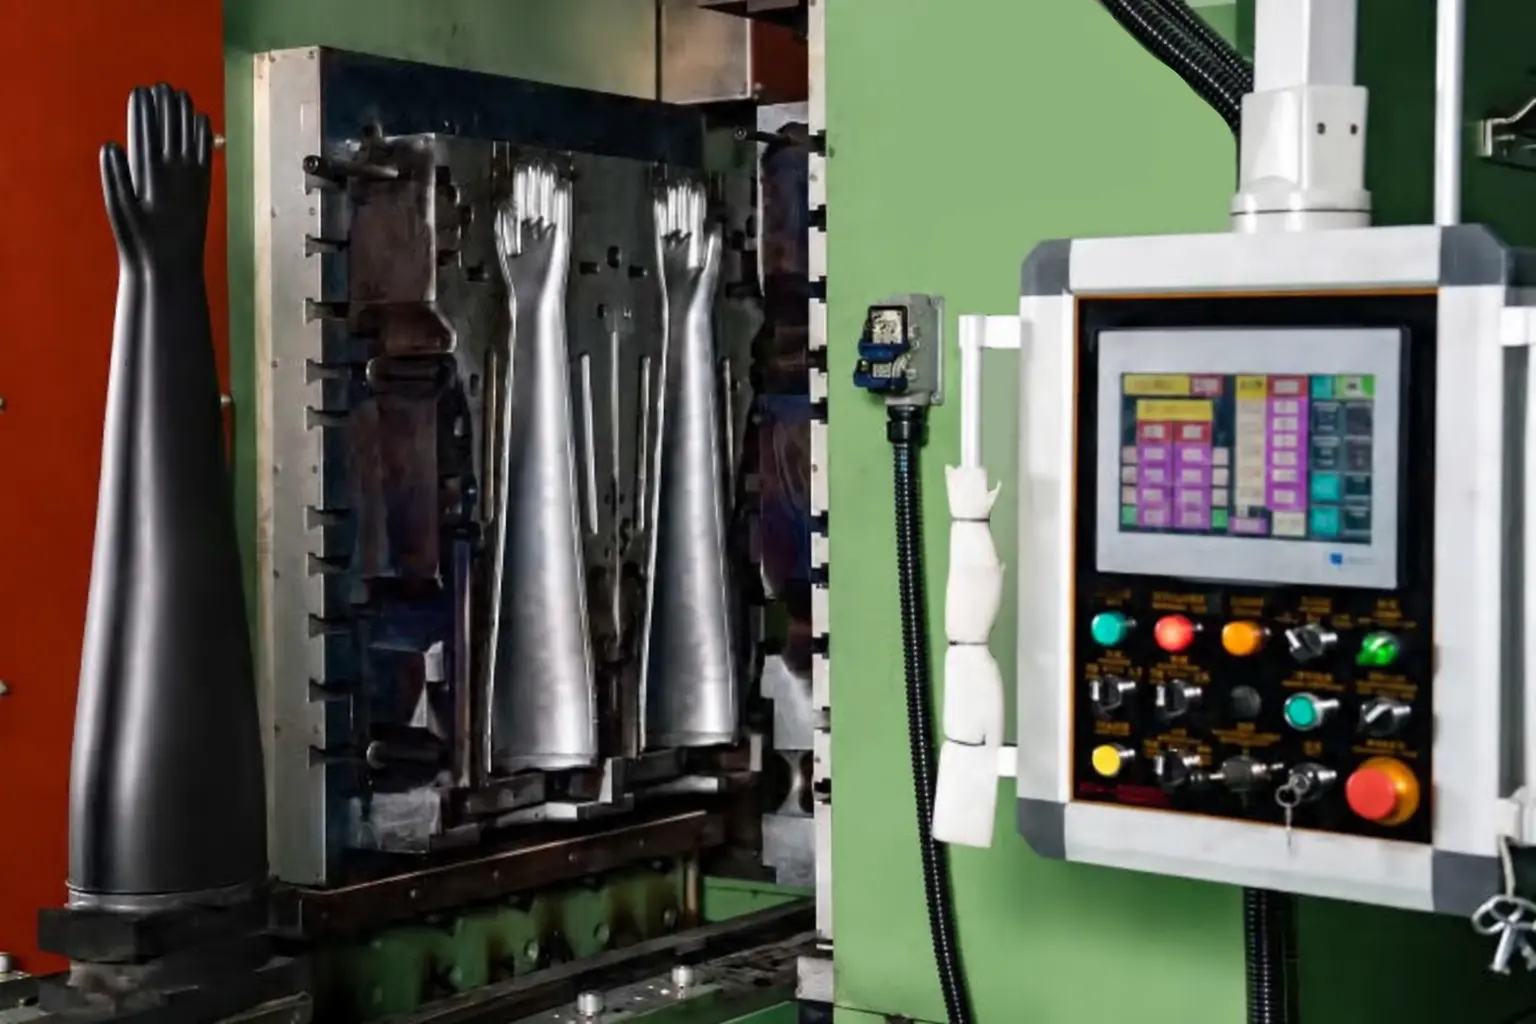
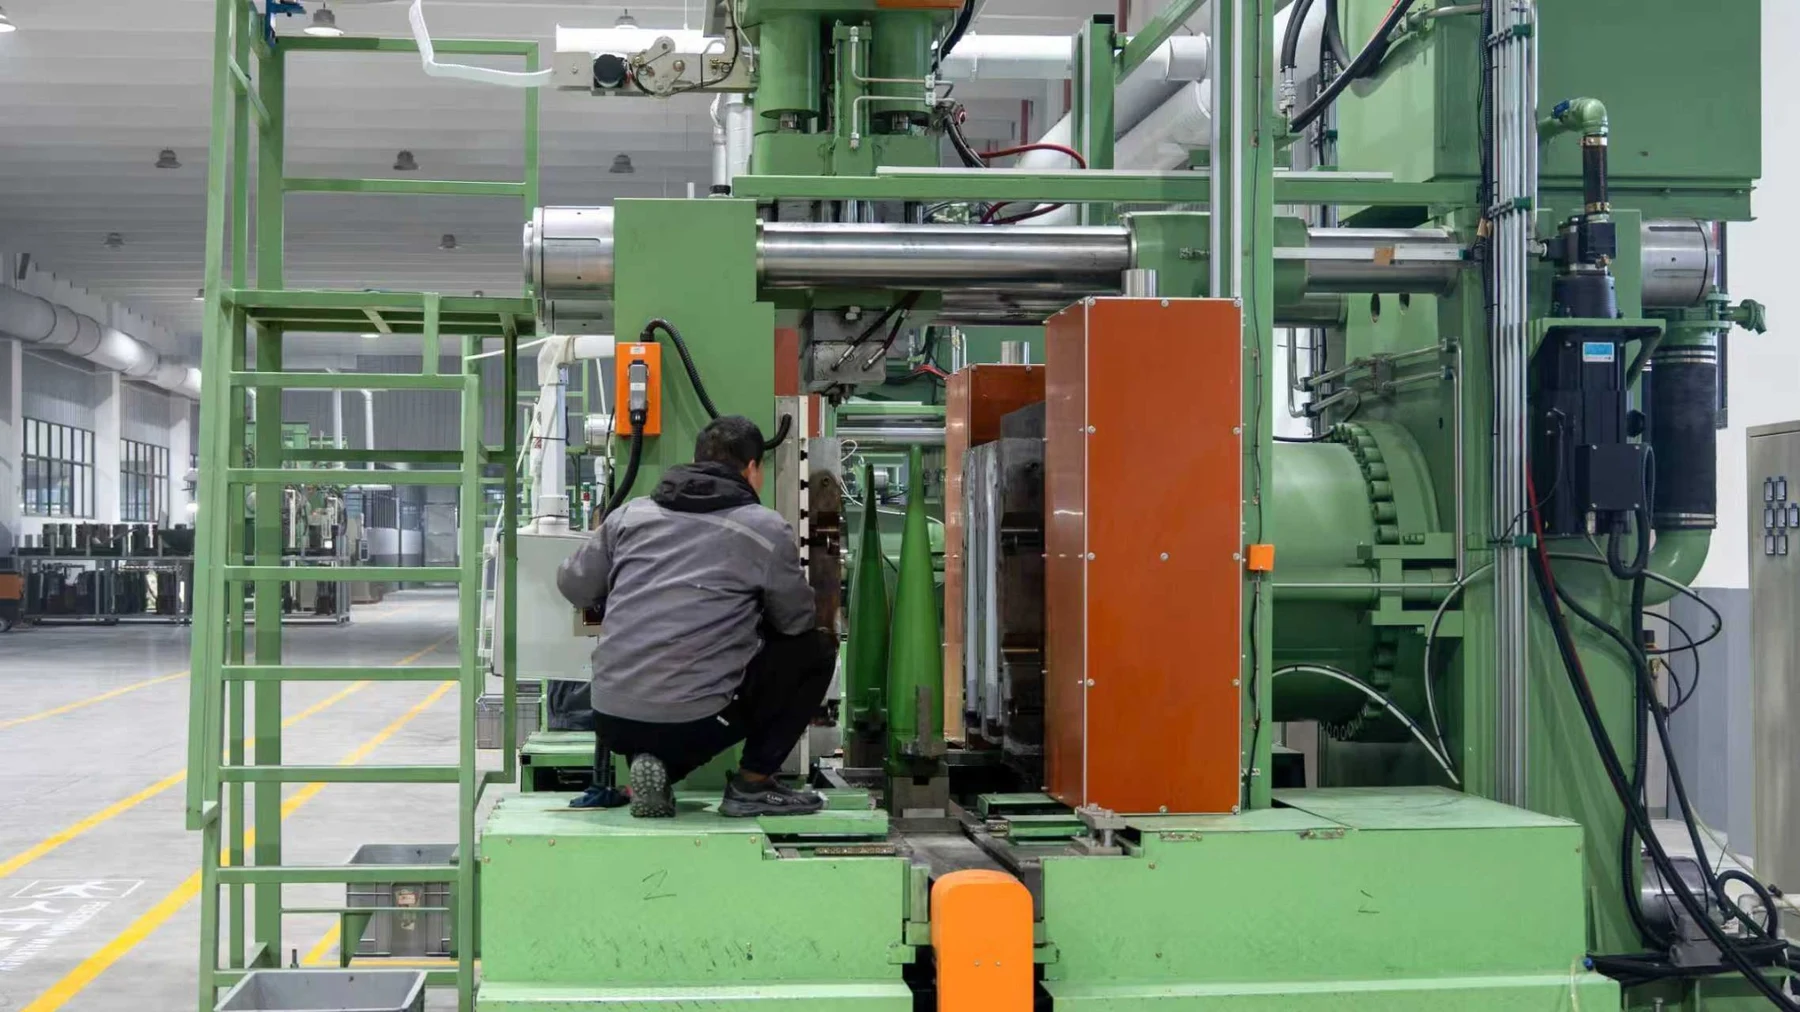
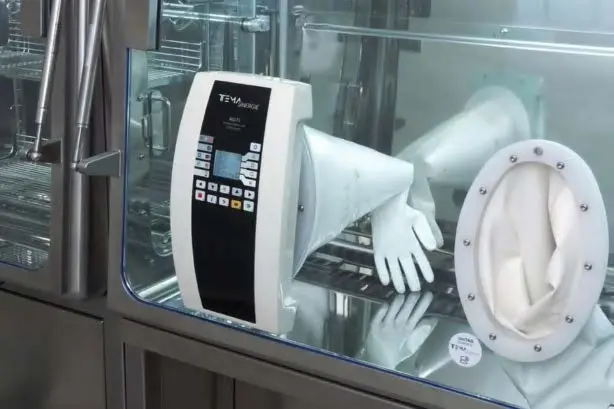
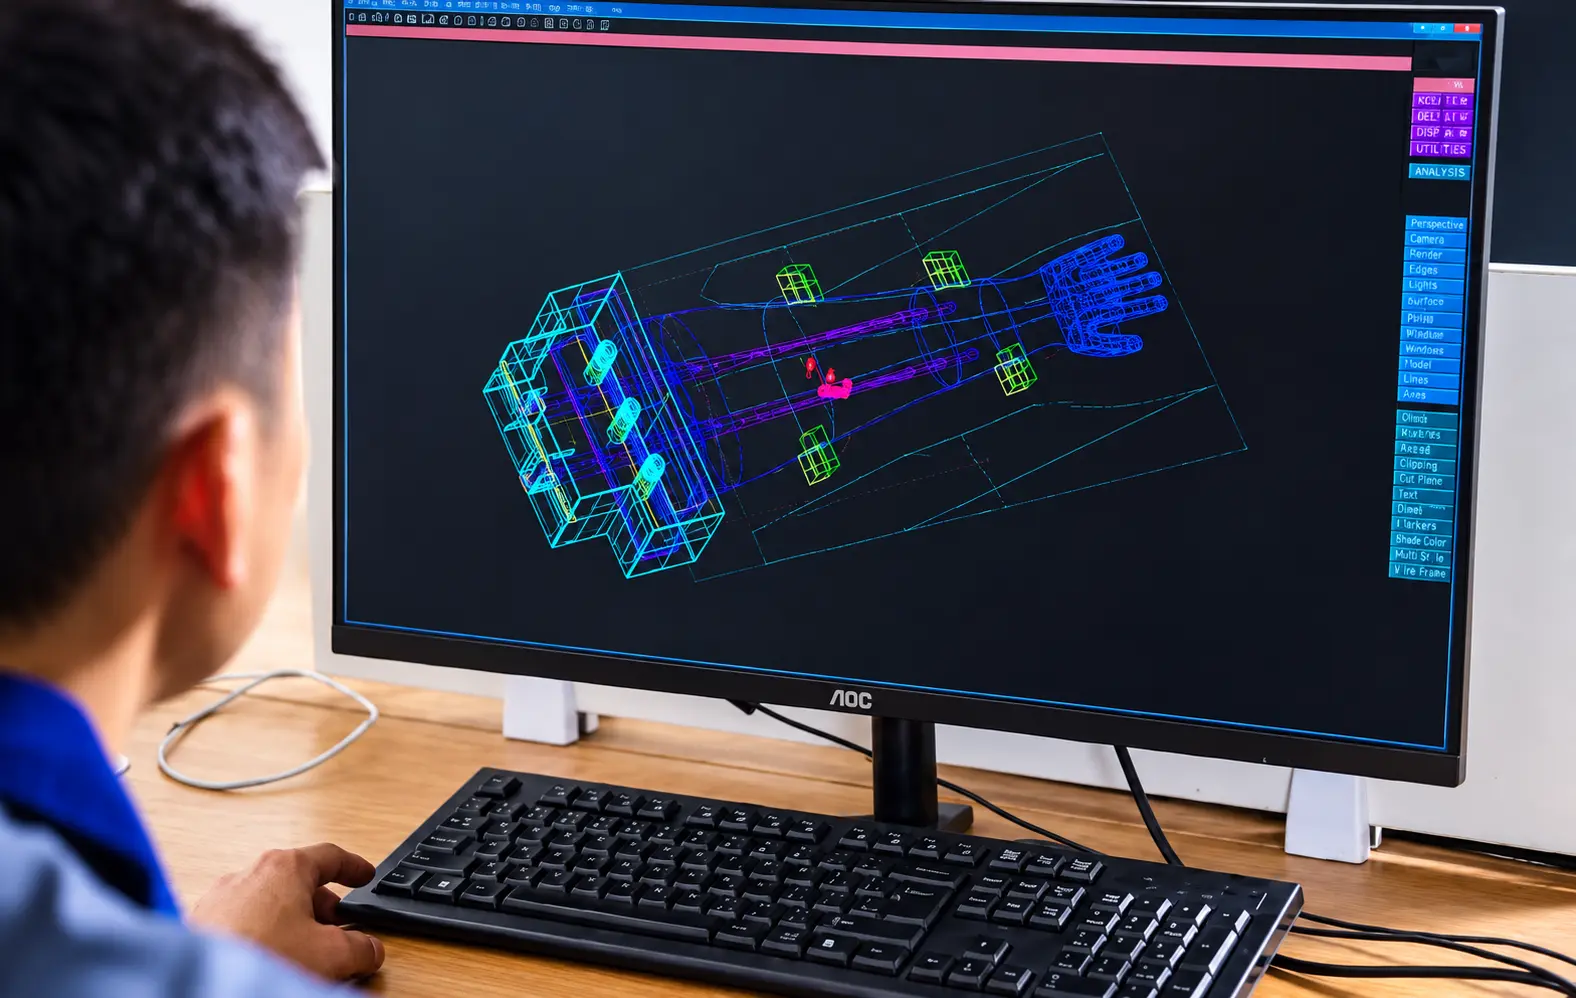
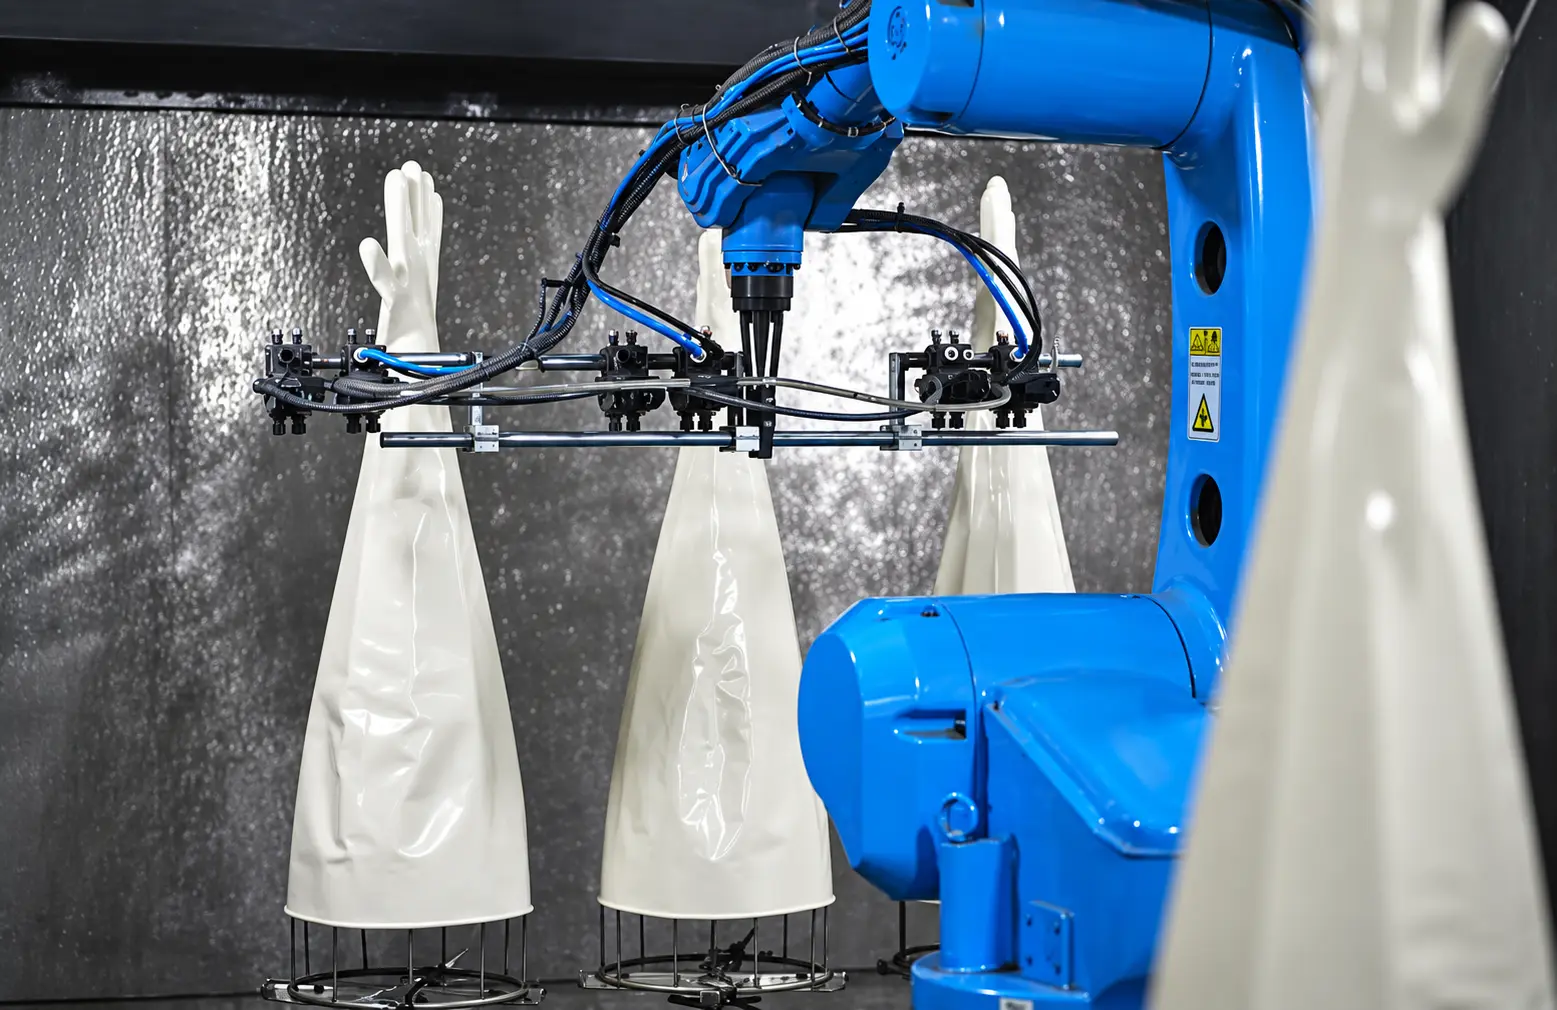
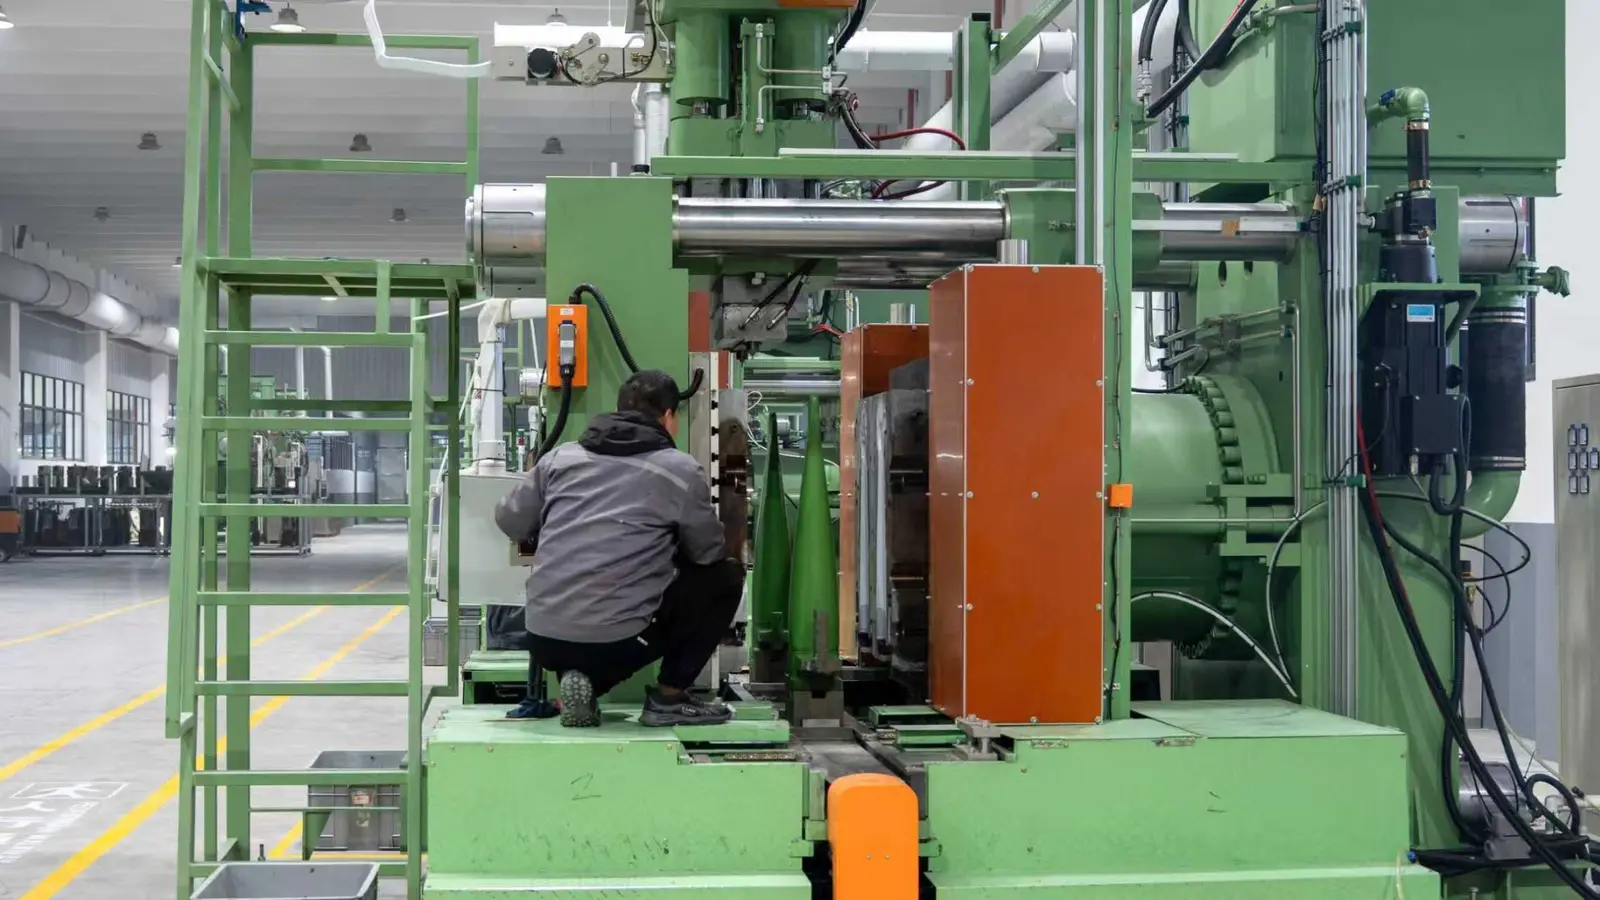
Kingsure isolator glove mold, molded glove and injection-compression machine control panel
Actual Kingsure tooling and process-control equipment
Technology leadership

Moving isolator gloves beyond the conventional dipping model.

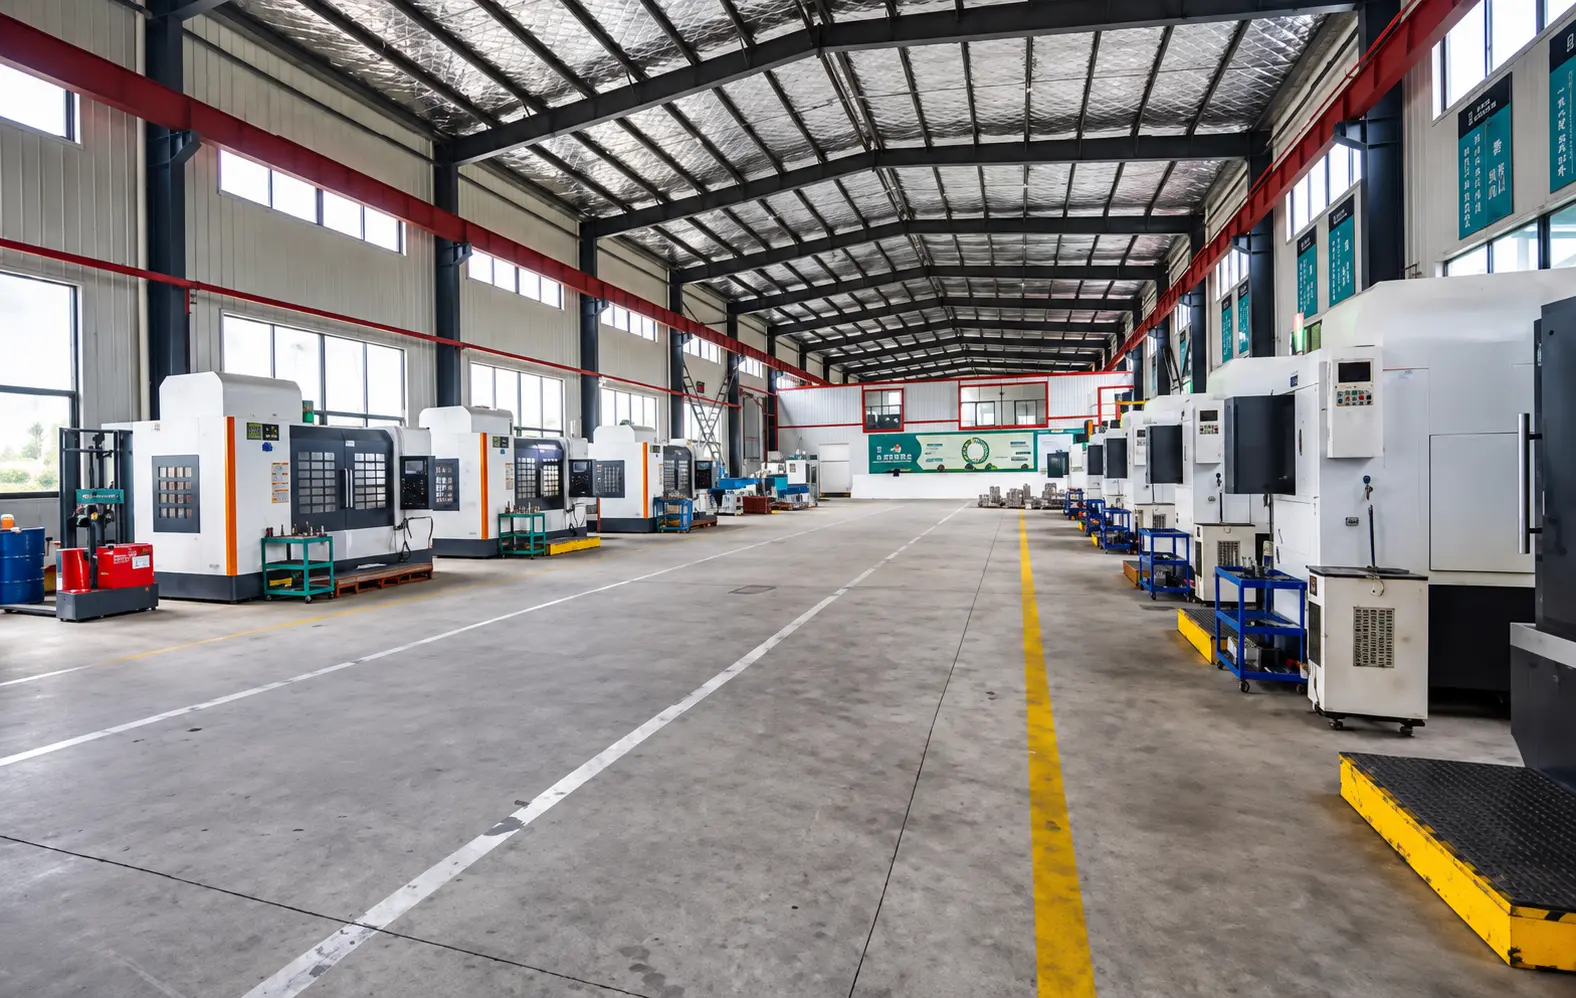
Kingsure injection-compression molding production equipment

Kingsure is the world’s first manufacturer to apply one-piece injection-compression molding to the scaled production of dry-box rubber gloves, replacing repeated liquid-bath film building with solid compound and dedicated closed tooling.
Two forming routes

Open-bath layer building versus closed-mold forming.

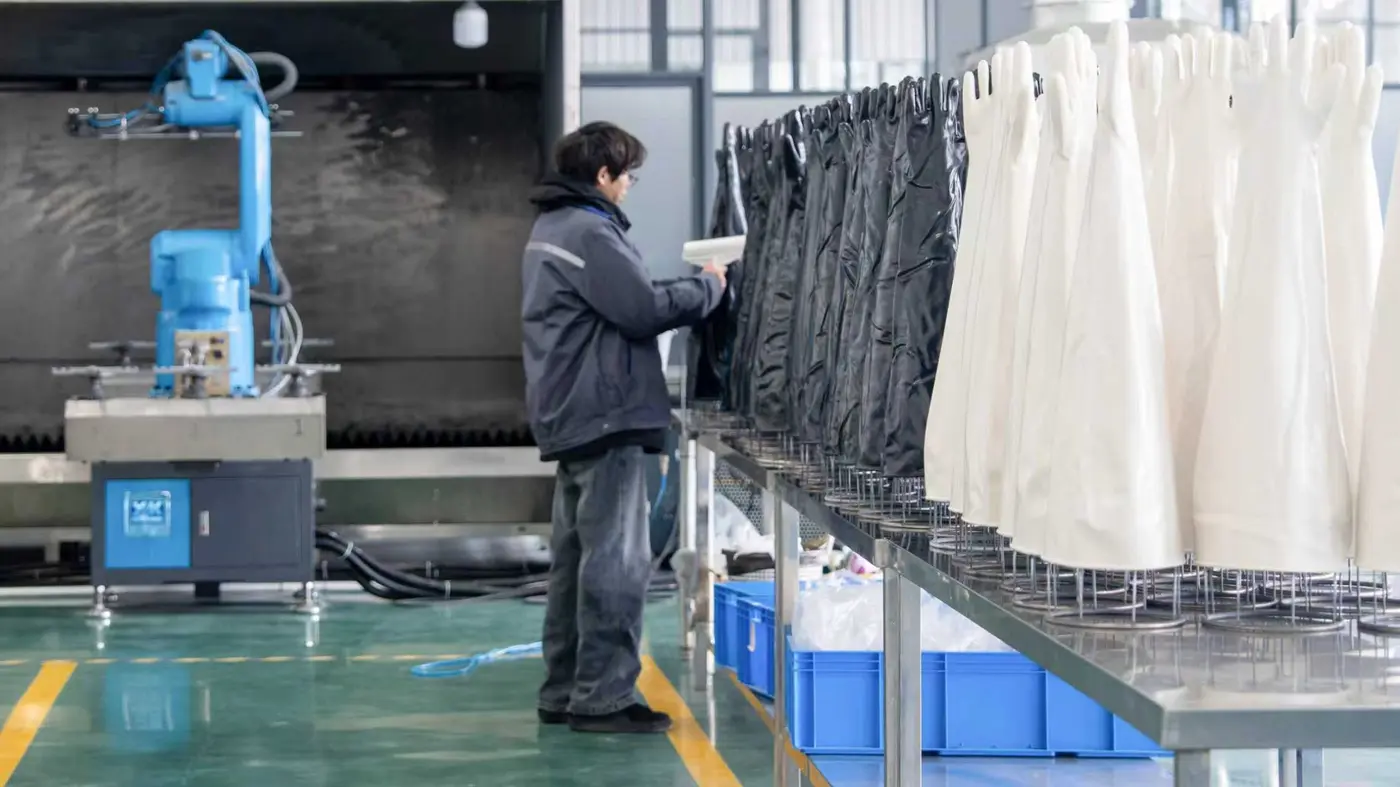
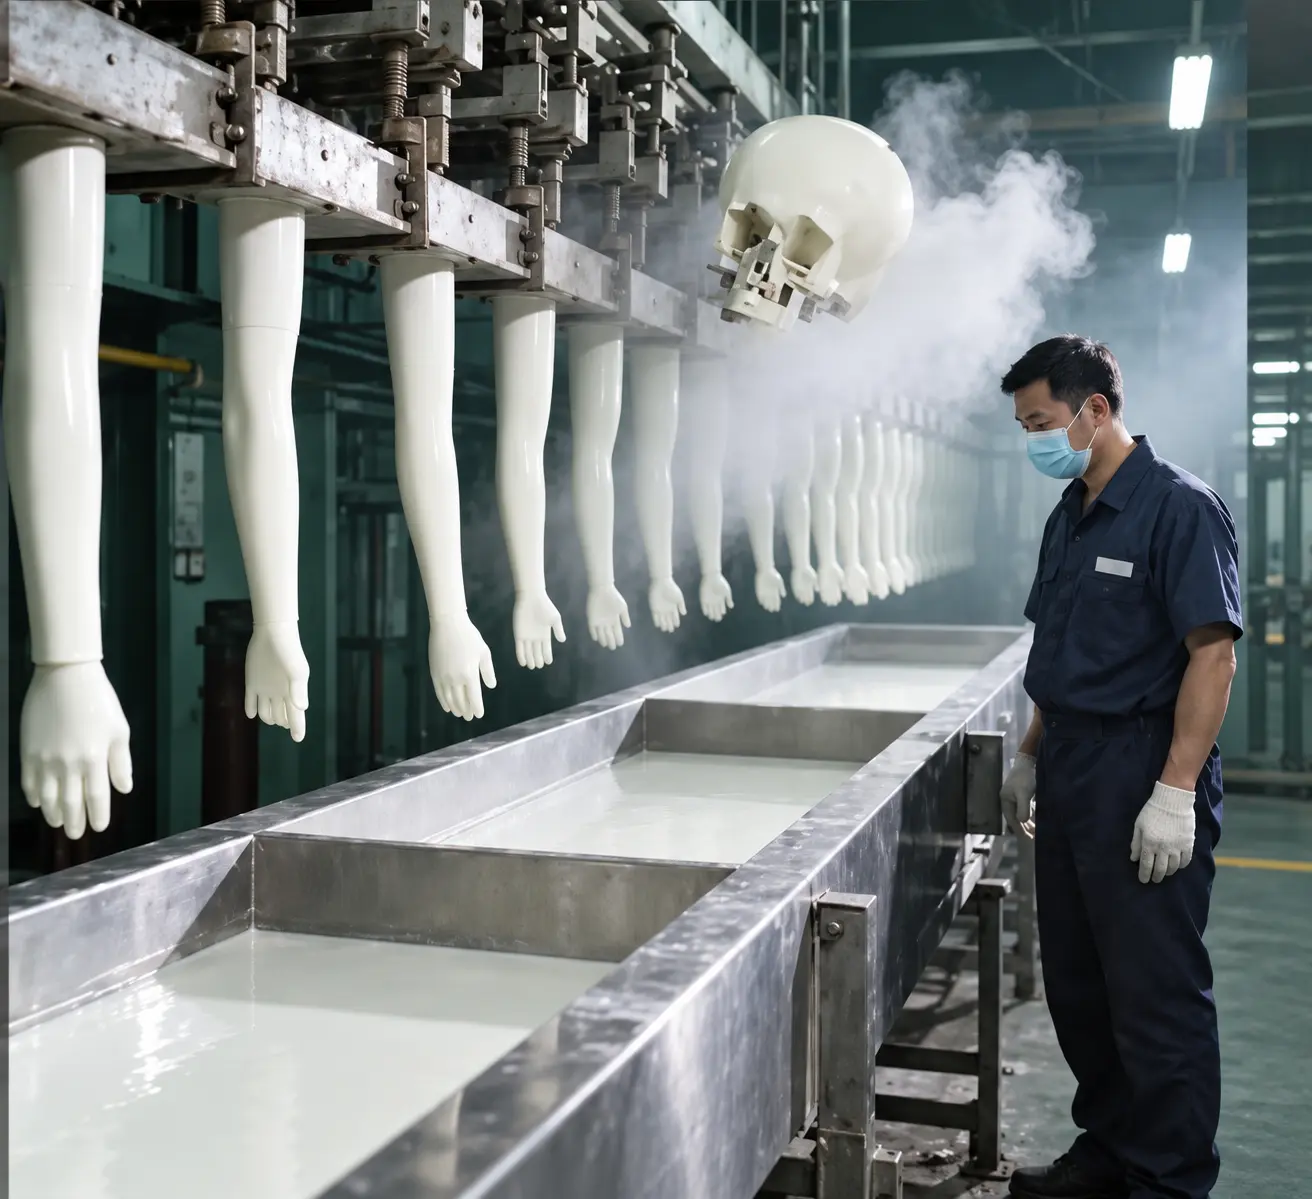
Conventional glove dipping line with hand formers above liquid tanks
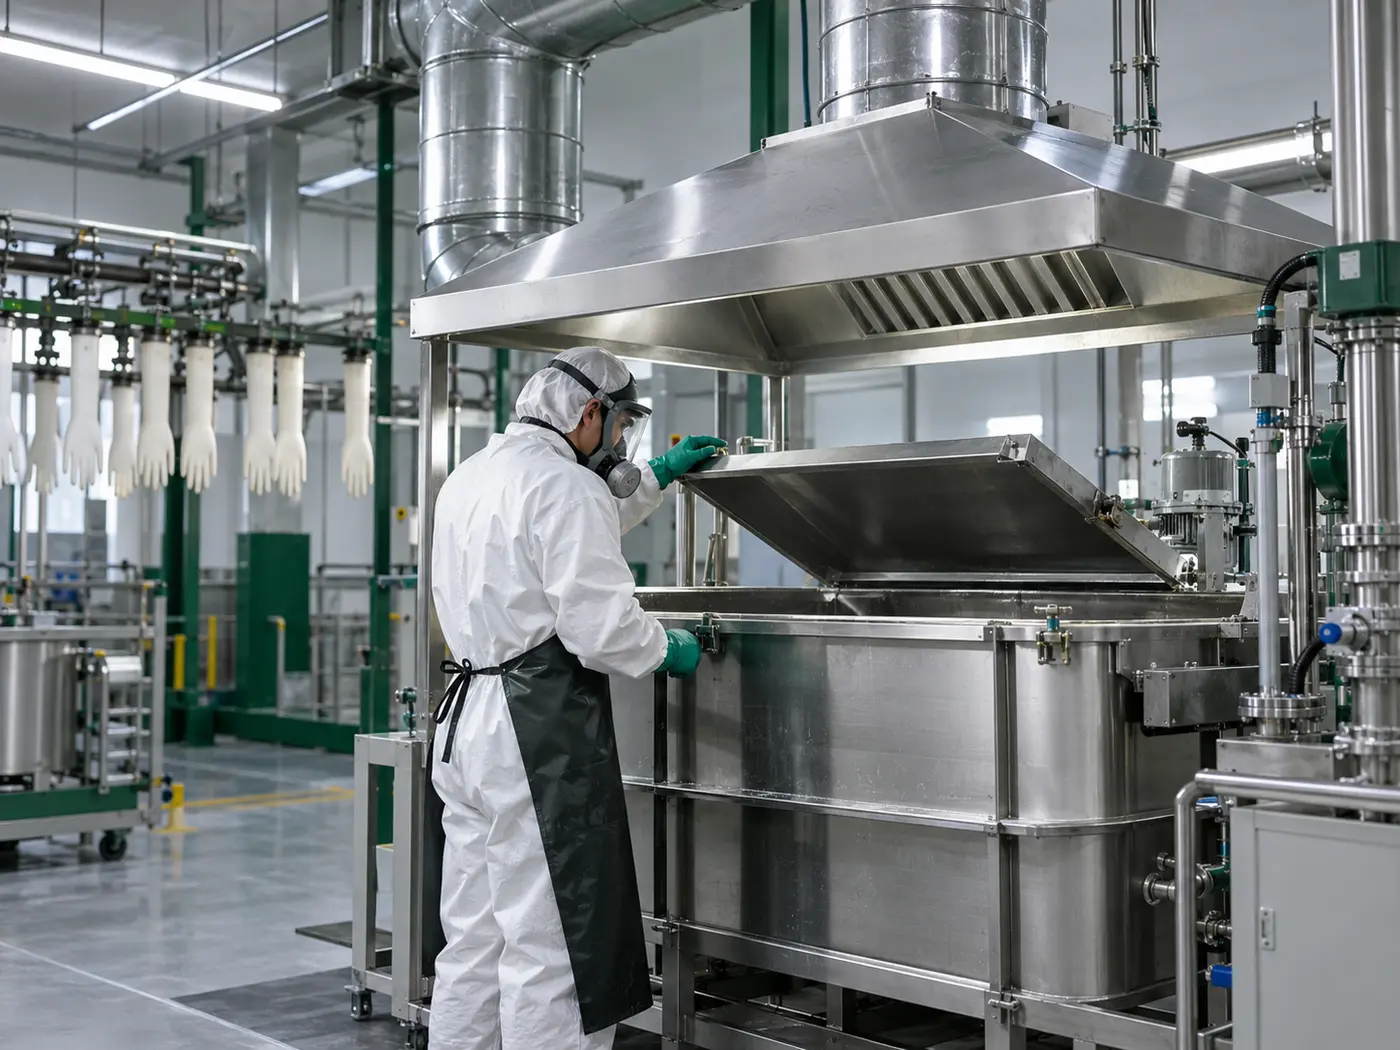
Conventional dipping routeLiquid compound is deposited on formers through repeated dipping, draining, drying and curing. Solvent-based cement requires large quantities of chemical solvent for preparation, storage, transfer and cleaning, creating worker-exposure, VOC-emission, fire-safety and solvent-bearing waste risks.
Kingsure closed glove mold and injection-compression process control panel
Kingsure one-piece injection-compression routeConventionally mixed solid rubber compound forms a complete glove inside dedicated closed tooling under controlled temperature, pressure and curing time. The forming process requires neither solvent-based dipping cement nor a large chemical-solvent preparation system, removing the associated pollution sources at their origin.
R&D background

Why Kingsure challenged solvent-based dipping.

Solvent is not only a formulation ingredient. Once introduced at scale, it creates an entire control system around storage, mixing, ventilation, fire safety, emissions and waste handling.

Industrial ventilation and VOC exposure controls in a solvent handling area
01

VOC and worker exposure

Volatile solvents can require local extraction, enclosed handling, exposure monitoring and off-gas treatment.
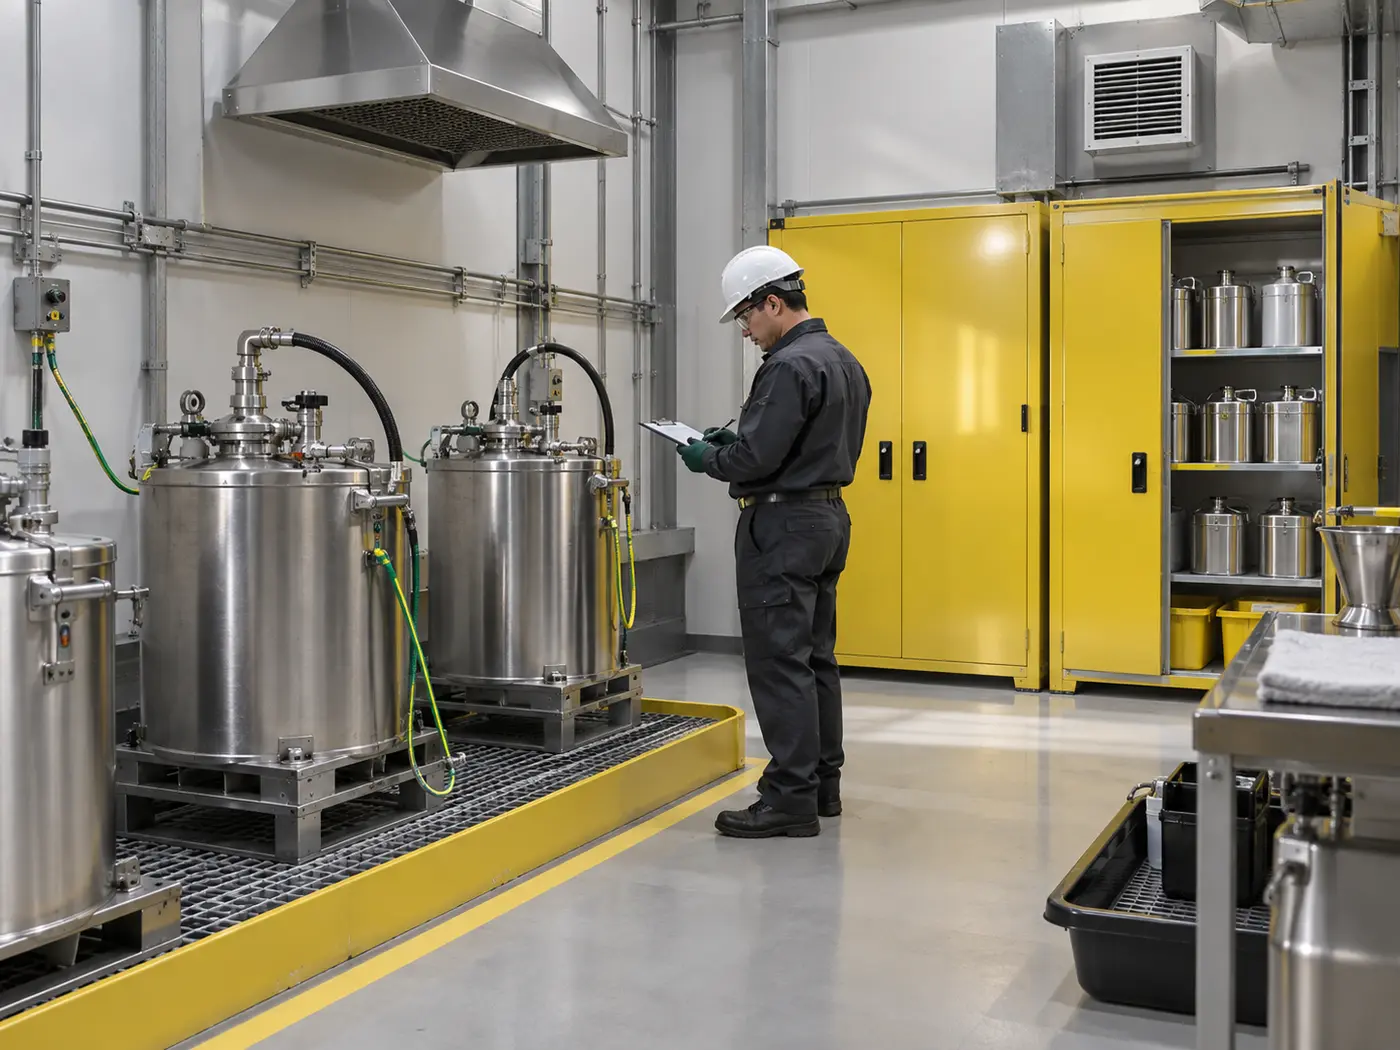
Controlled flammable liquid storage with fire protection measures
02

Fire and storage controls

Flammable liquids add requirements for classified storage, transfer, grounding, ignition control and emergency response.
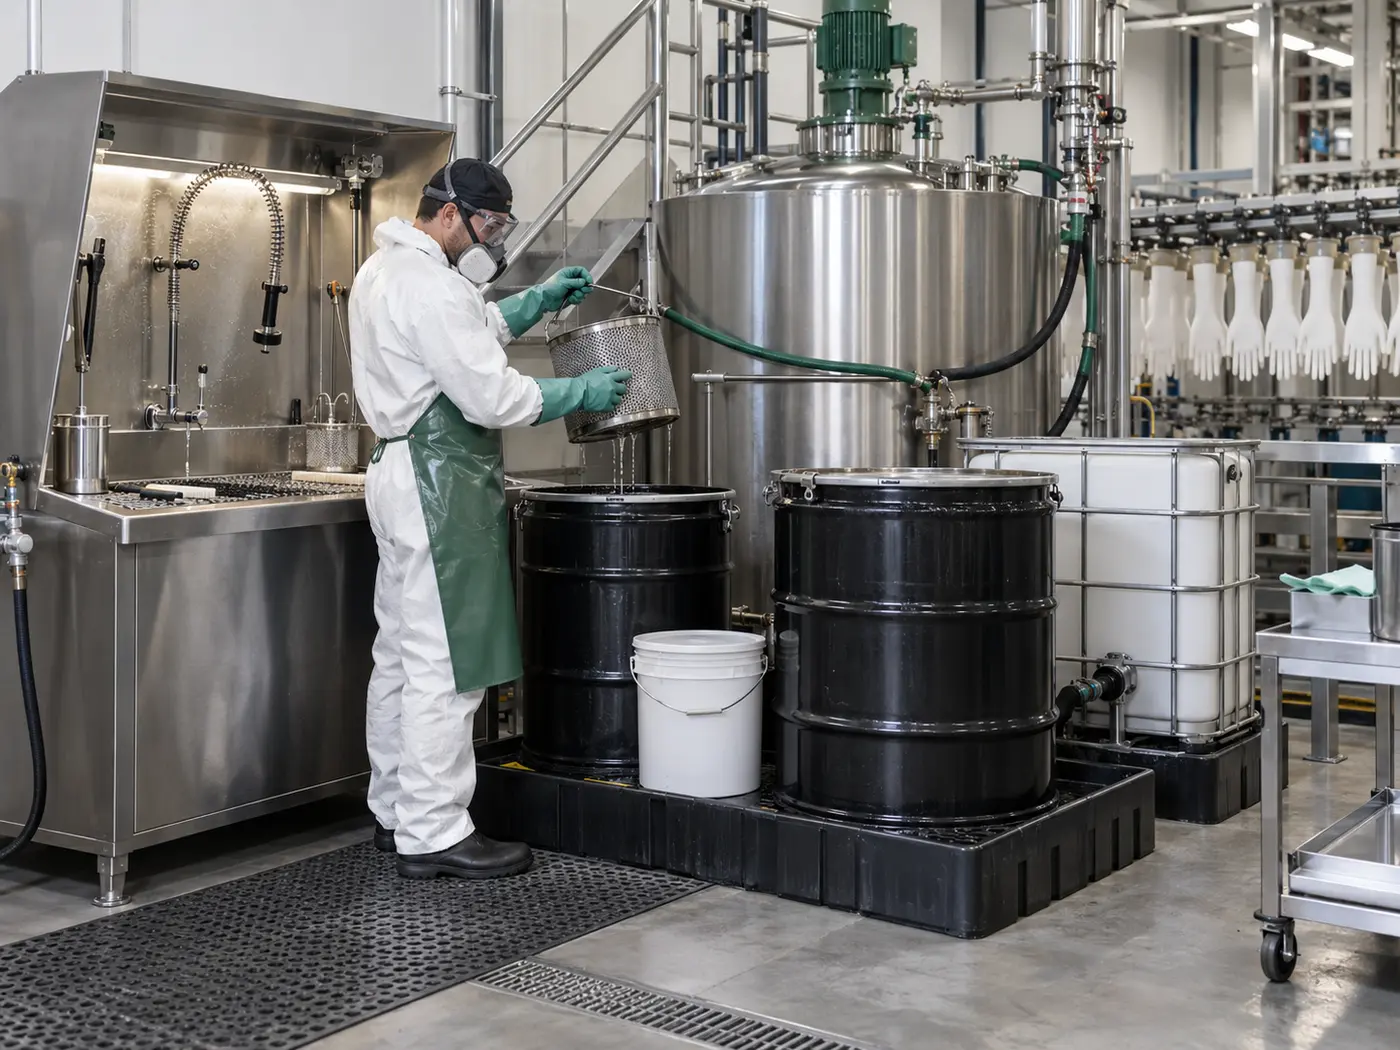
Industrial solvent cleaning and waste stream management
03

Cleaning and waste streams

Tank changeovers, residue and cleaning materials create additional solvent-bearing waste that must be controlled.
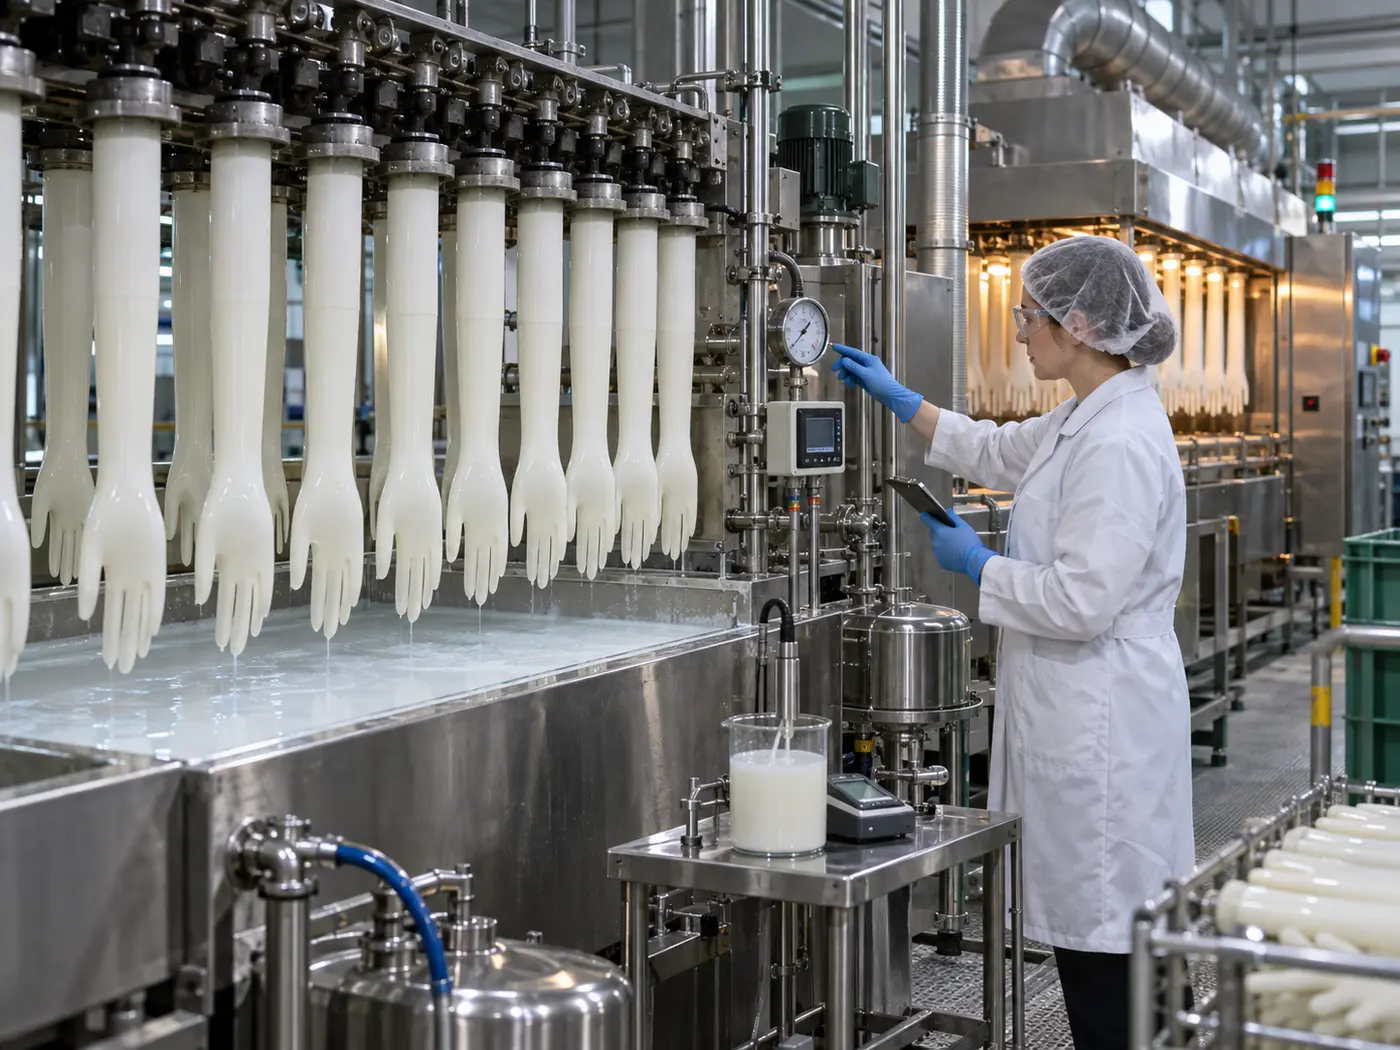
Process engineer monitoring interacting production variables
04

Many interacting variables

Bath viscosity, solids, former temperature, withdrawal speed, ambient conditions and drying all affect the deposited film.

Engineering objective

Kingsure’s objective was not to call a conventional line “greener,” but to remove the repeated liquid-bath forming mechanism itself and rebuild the process around solid compound and closed tooling.

Controlled manufacturing sequence

From compound verification to finished-glove release.

Control is concentrated on compound condition, tooling, injection-compression parameters, curing, demolding and documented batch verification.
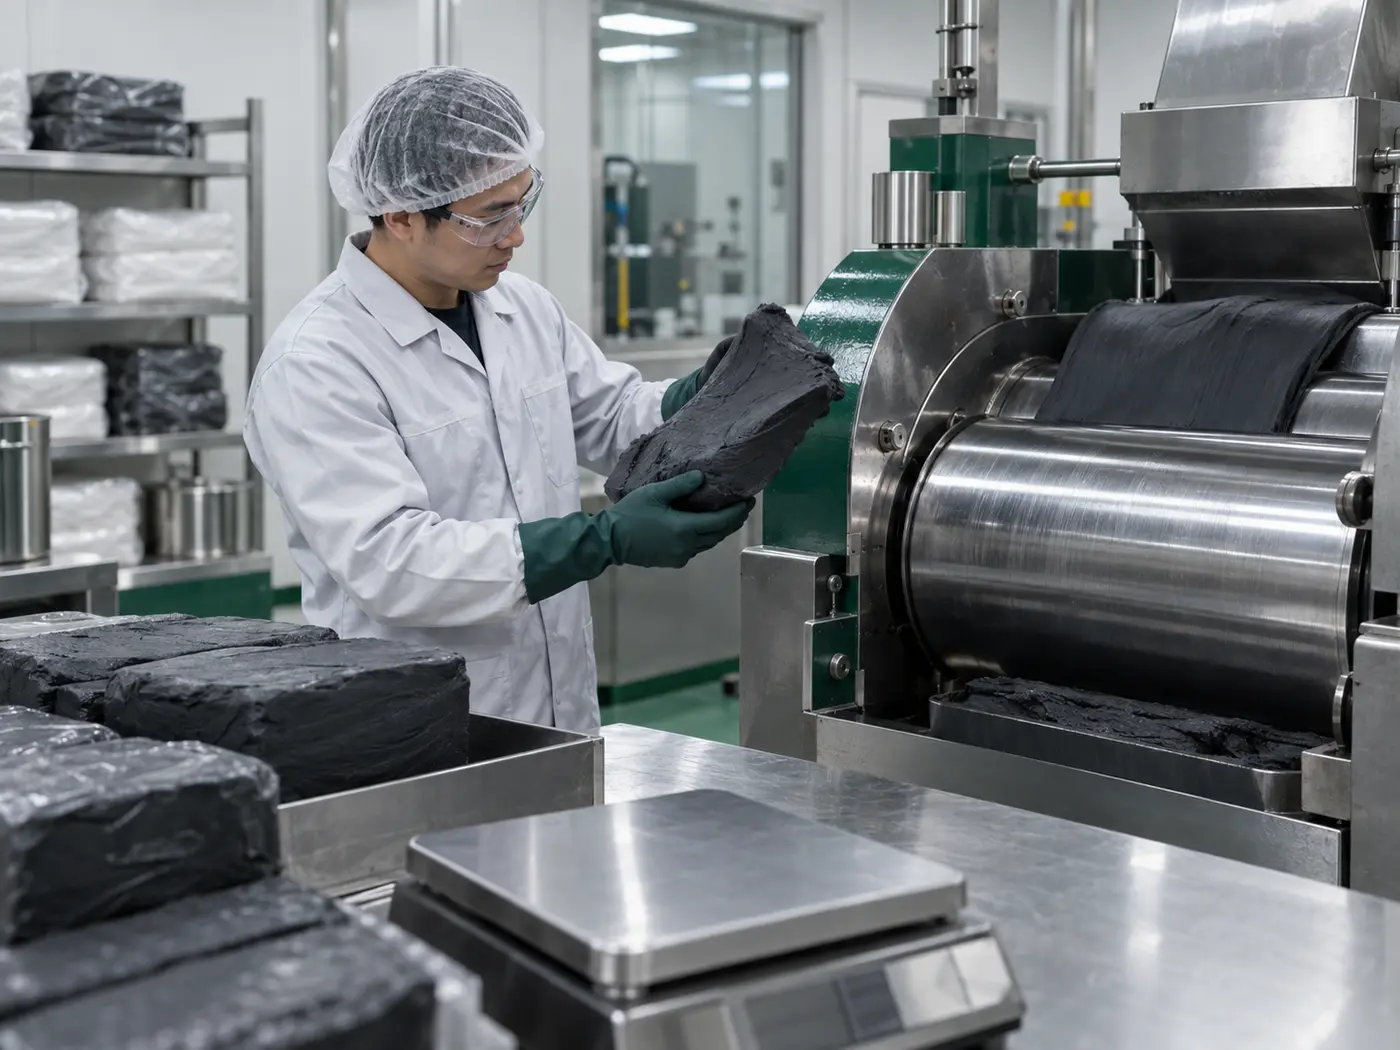
Solid rubber compound preparation and verification
01

Compound preparation

The rubber formulation is mixed, conditioned and verified before forming.
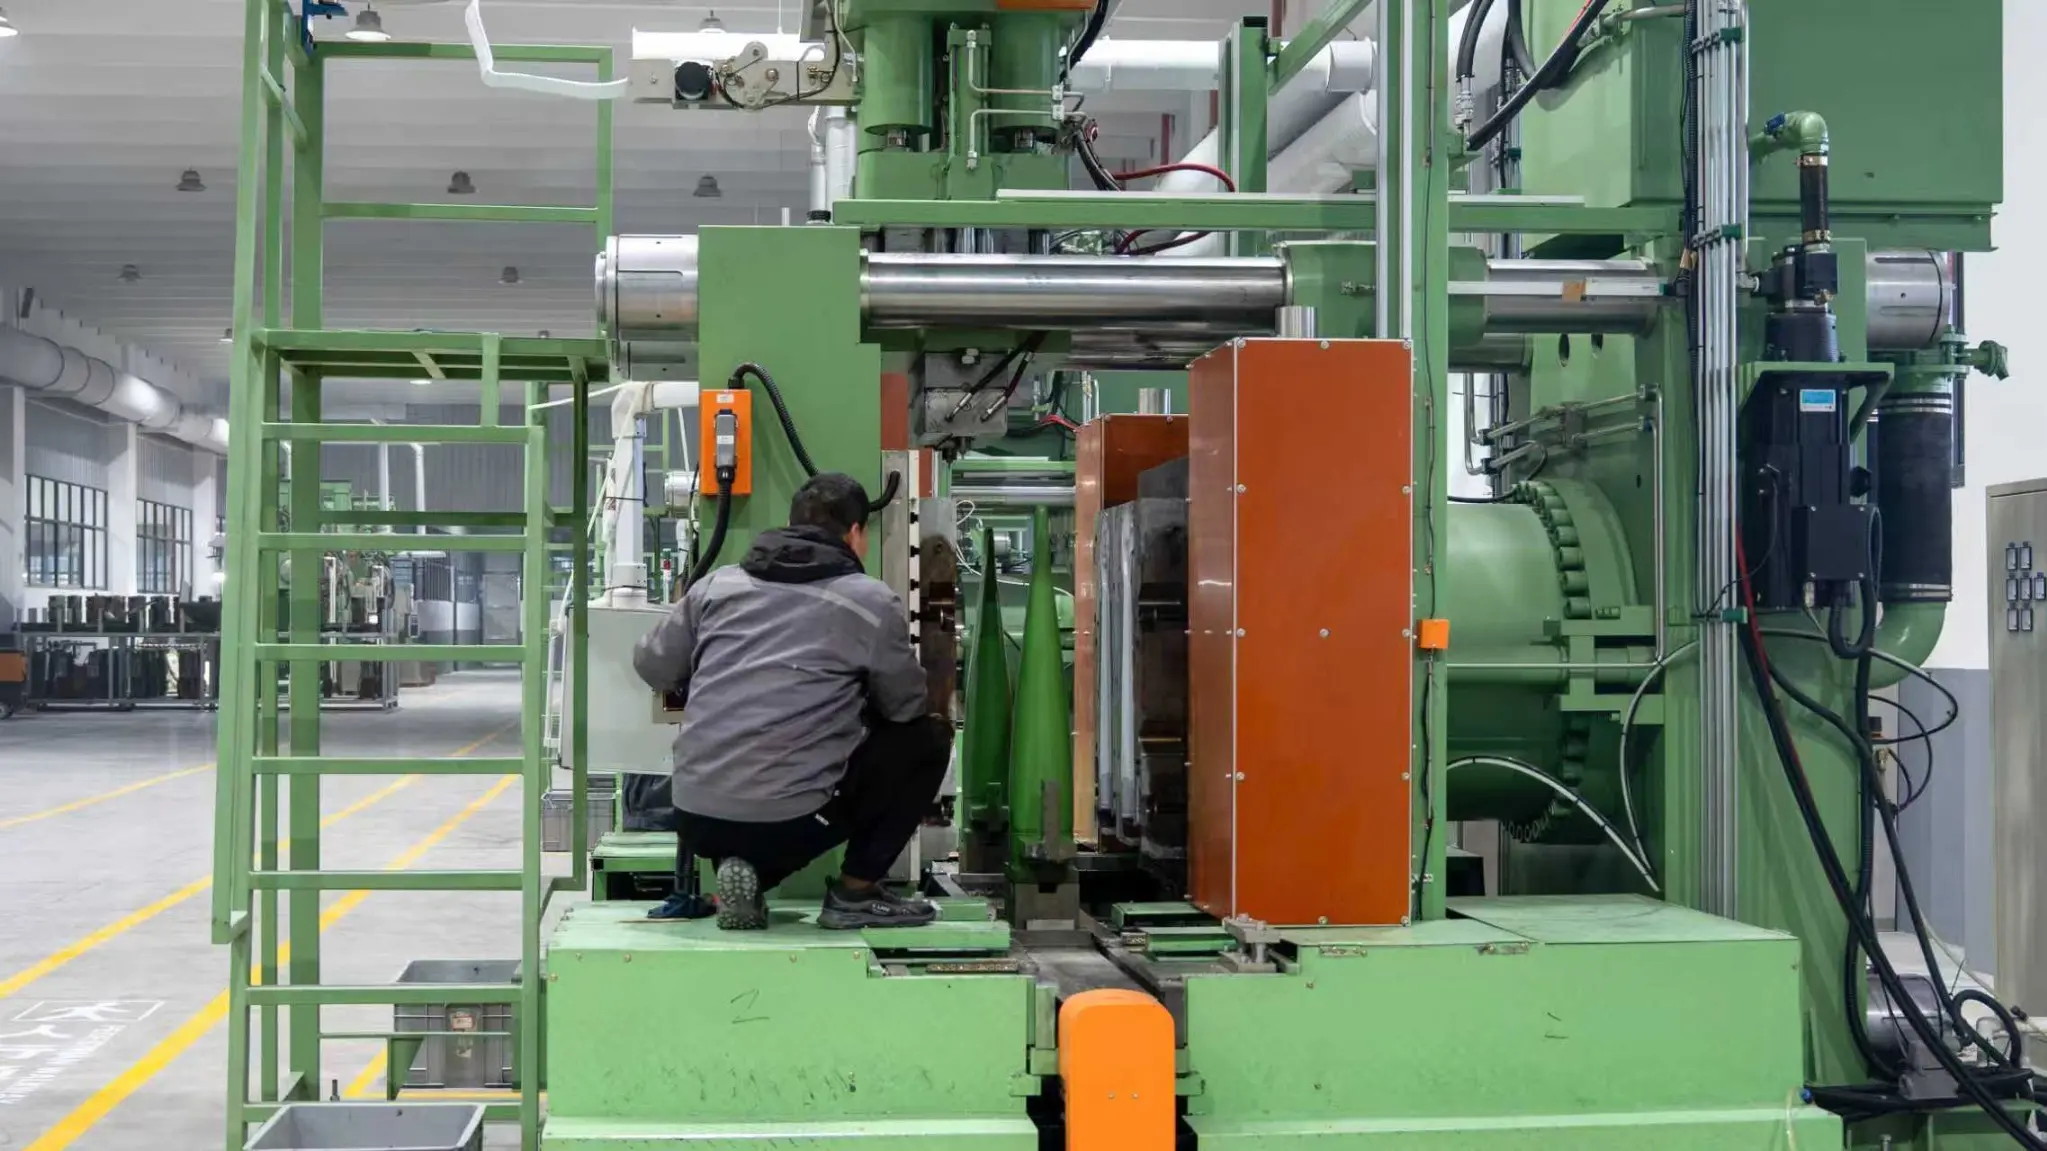
Dedicated closed mold preparation and inspection
02

Tool preparation

Cavity condition, cleanliness and critical tooling surfaces are confirmed.
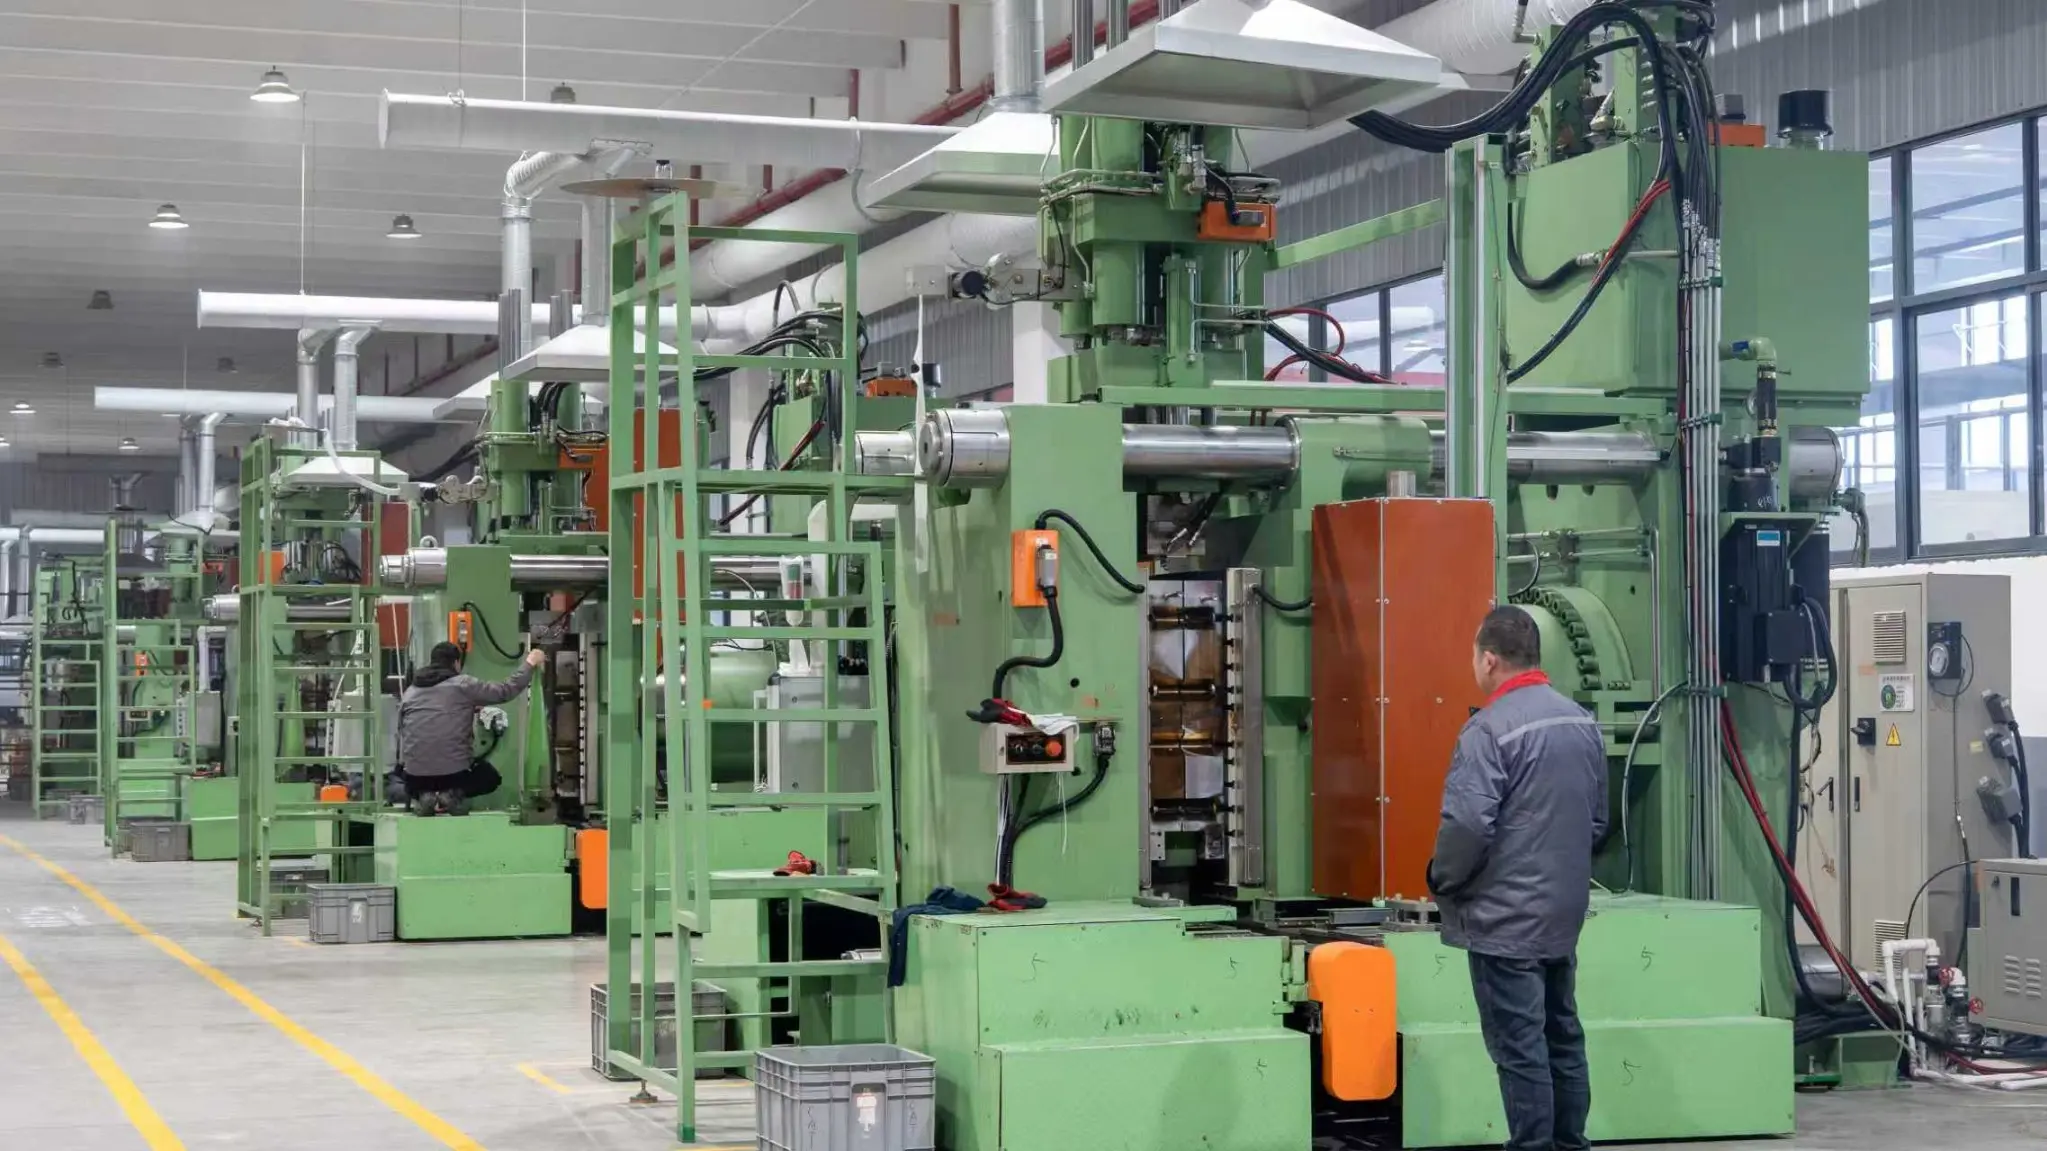
Injection-compression forming in closed glove tooling
03

Injection-compression forming

Compound fills the closed cavity under controlled pressure and temperature.
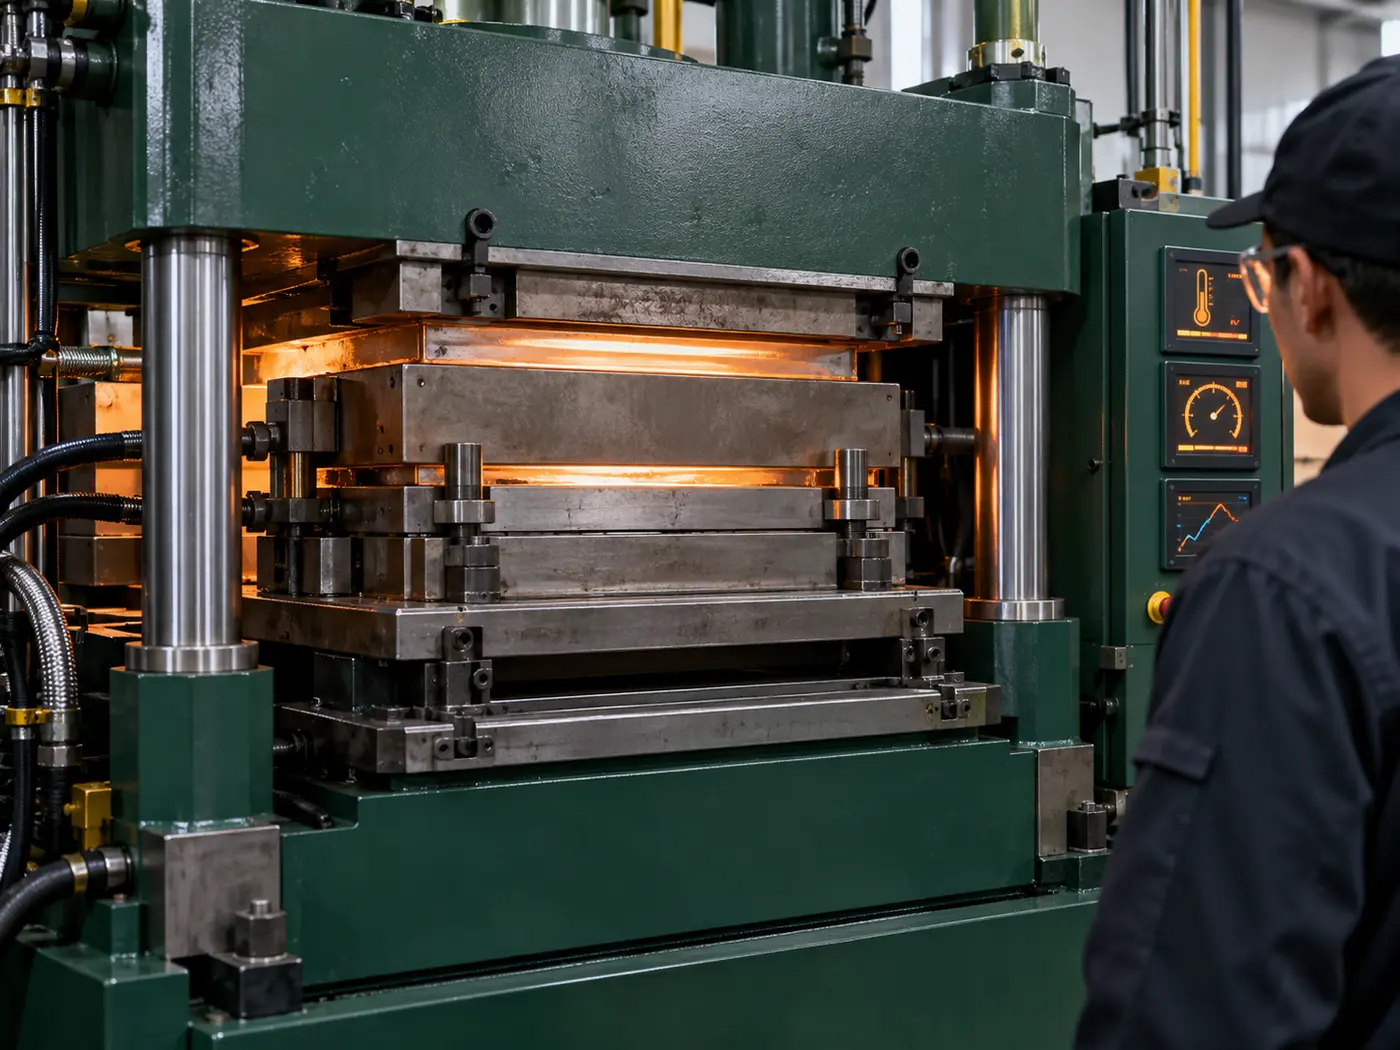
Controlled thermal curing of the molded glove
04

Curing

Time and thermal history are managed to develop the required properties.
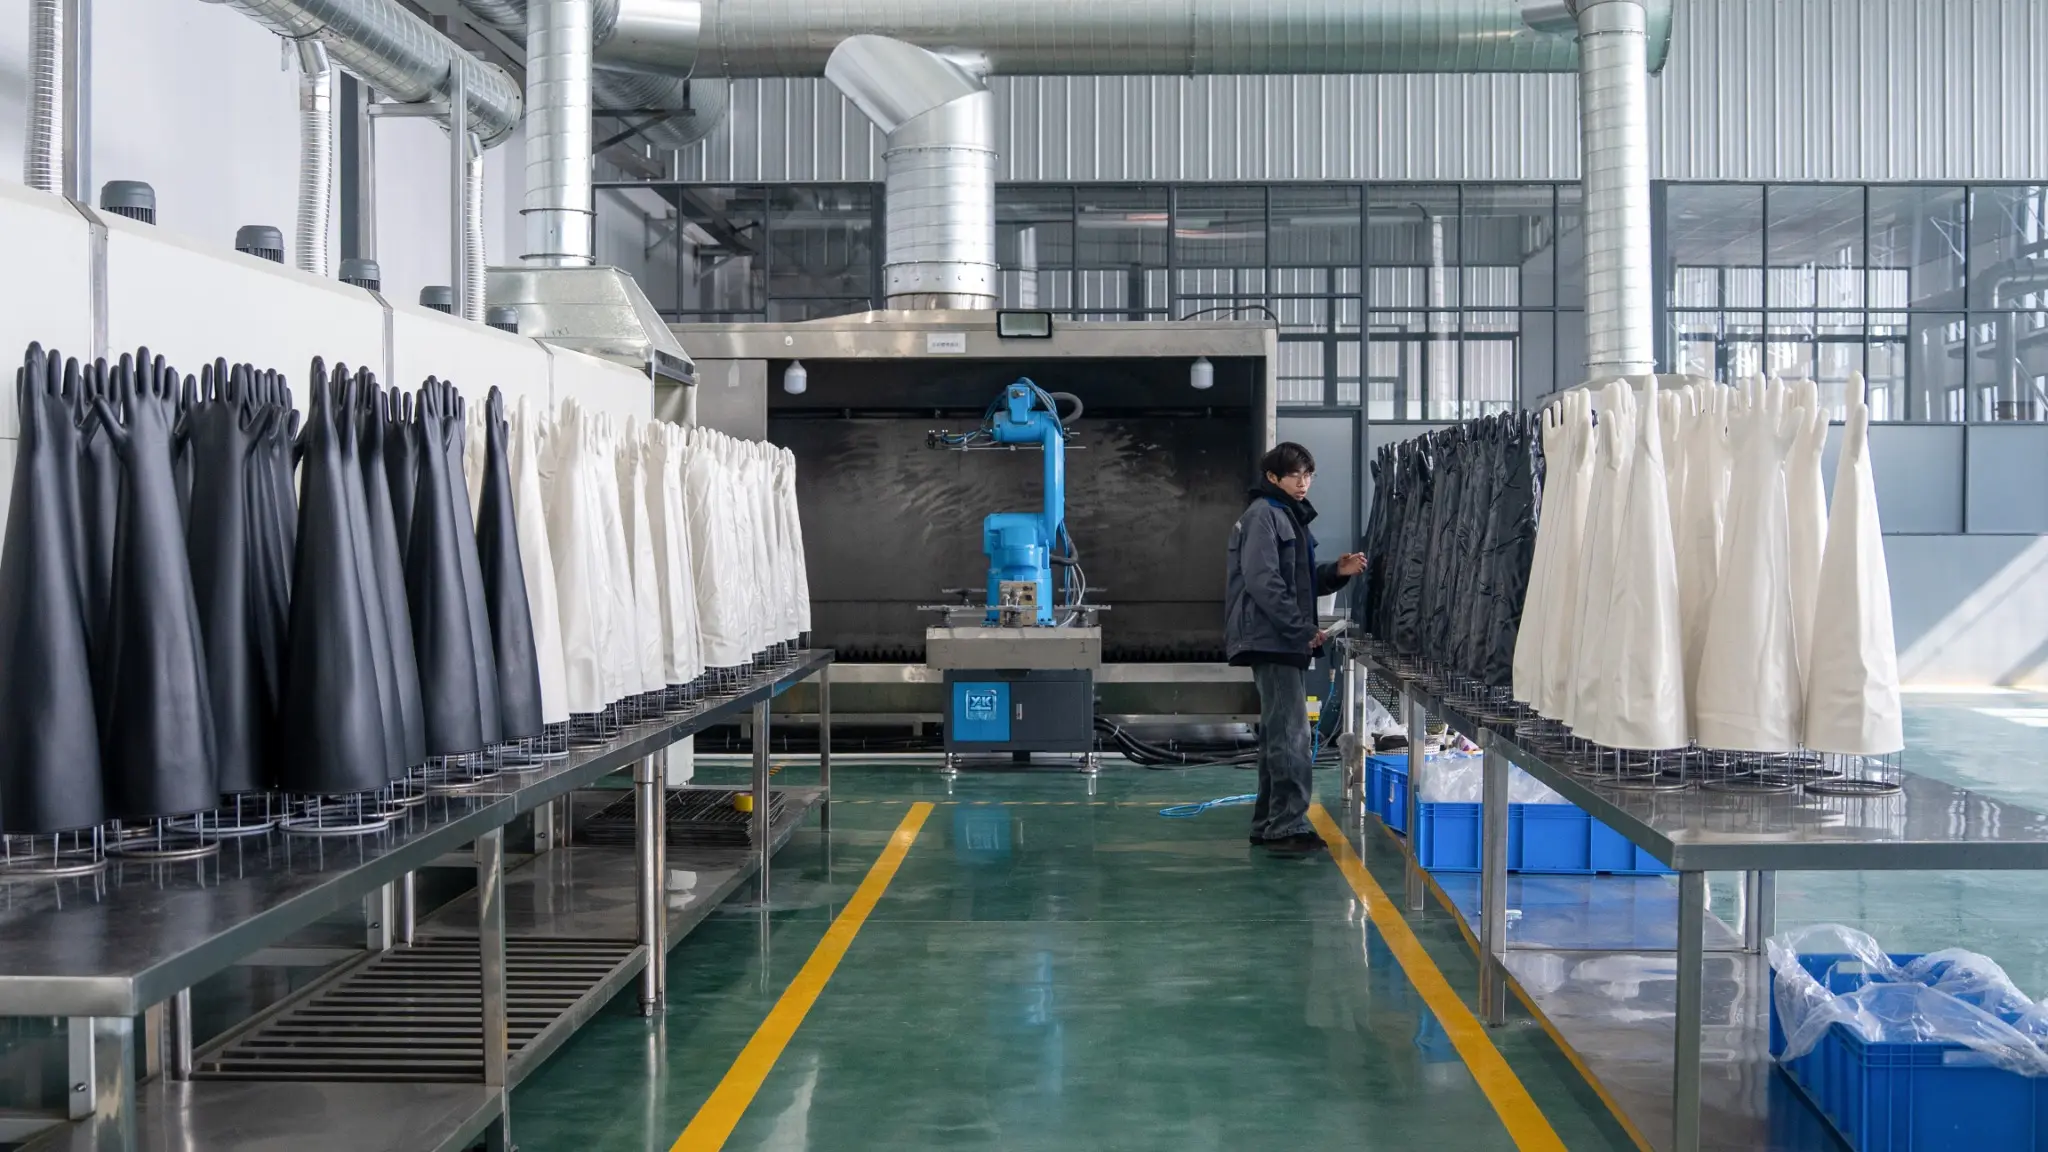
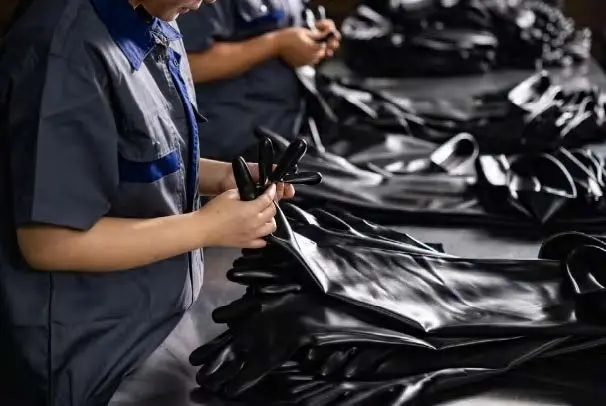
Glove demolding, finishing and visual examination
05

Demolding and finishing

The continuous glove is removed, finished and visually examined.
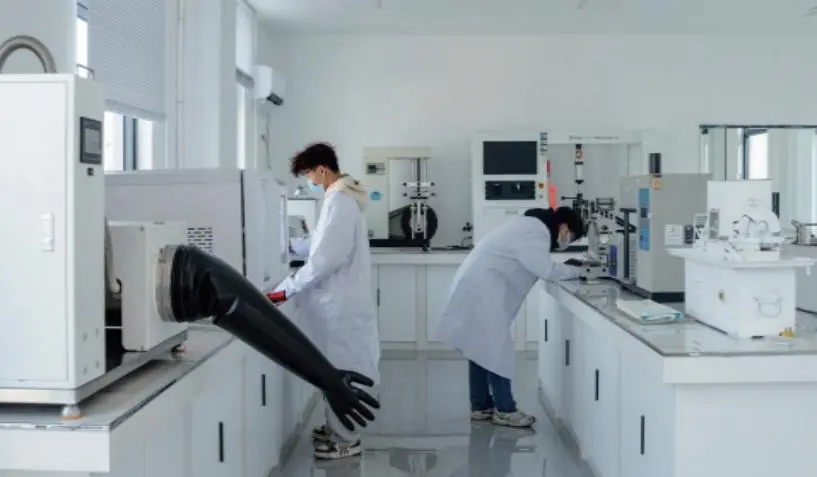
Laboratory batch inspection and release testing
06

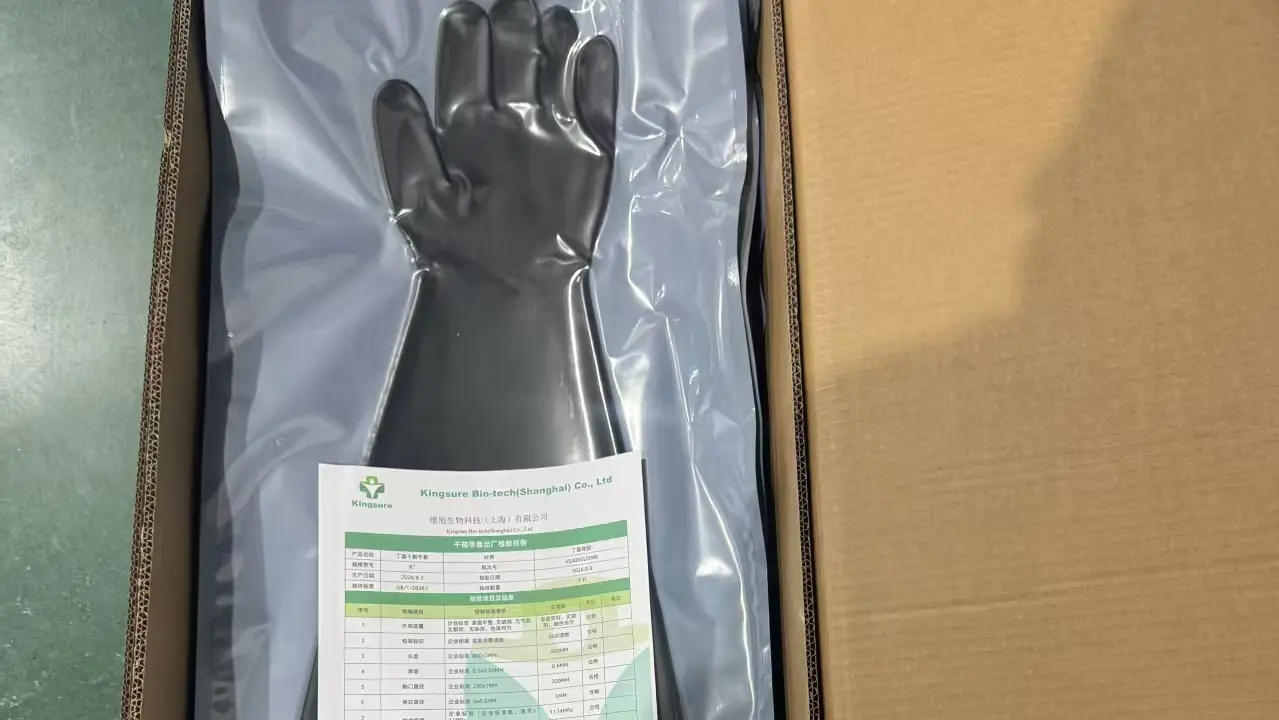
Batch inspection and release

Representative samples from every production batch are tested and recorded before release.
Designed into the mold

Geometry, thickness and reinforcement become engineering variables.

In a dipping process, film build is strongly influenced by liquid behavior and repeated coating conditions. In Kingsure’s route, the dedicated cavity defines the principal glove geometry, while controlled material charge and molding parameters support repeatability.

  • One continuous hand, finger, sleeve and cuff structure
  • Targeted reinforcement can be built into defined high-stress zones
  • Critical dimensions and nominal thickness are verified against documented criteria
  • Mold, batch, process and inspection records support traceability
Inspection in practice

Checks from production to final release.

Real inspection and testing views from the Kingsure manufacturing and laboratory workflow.